

Metal Detector for Conveyor Belt Systems
2026-09-01 16:48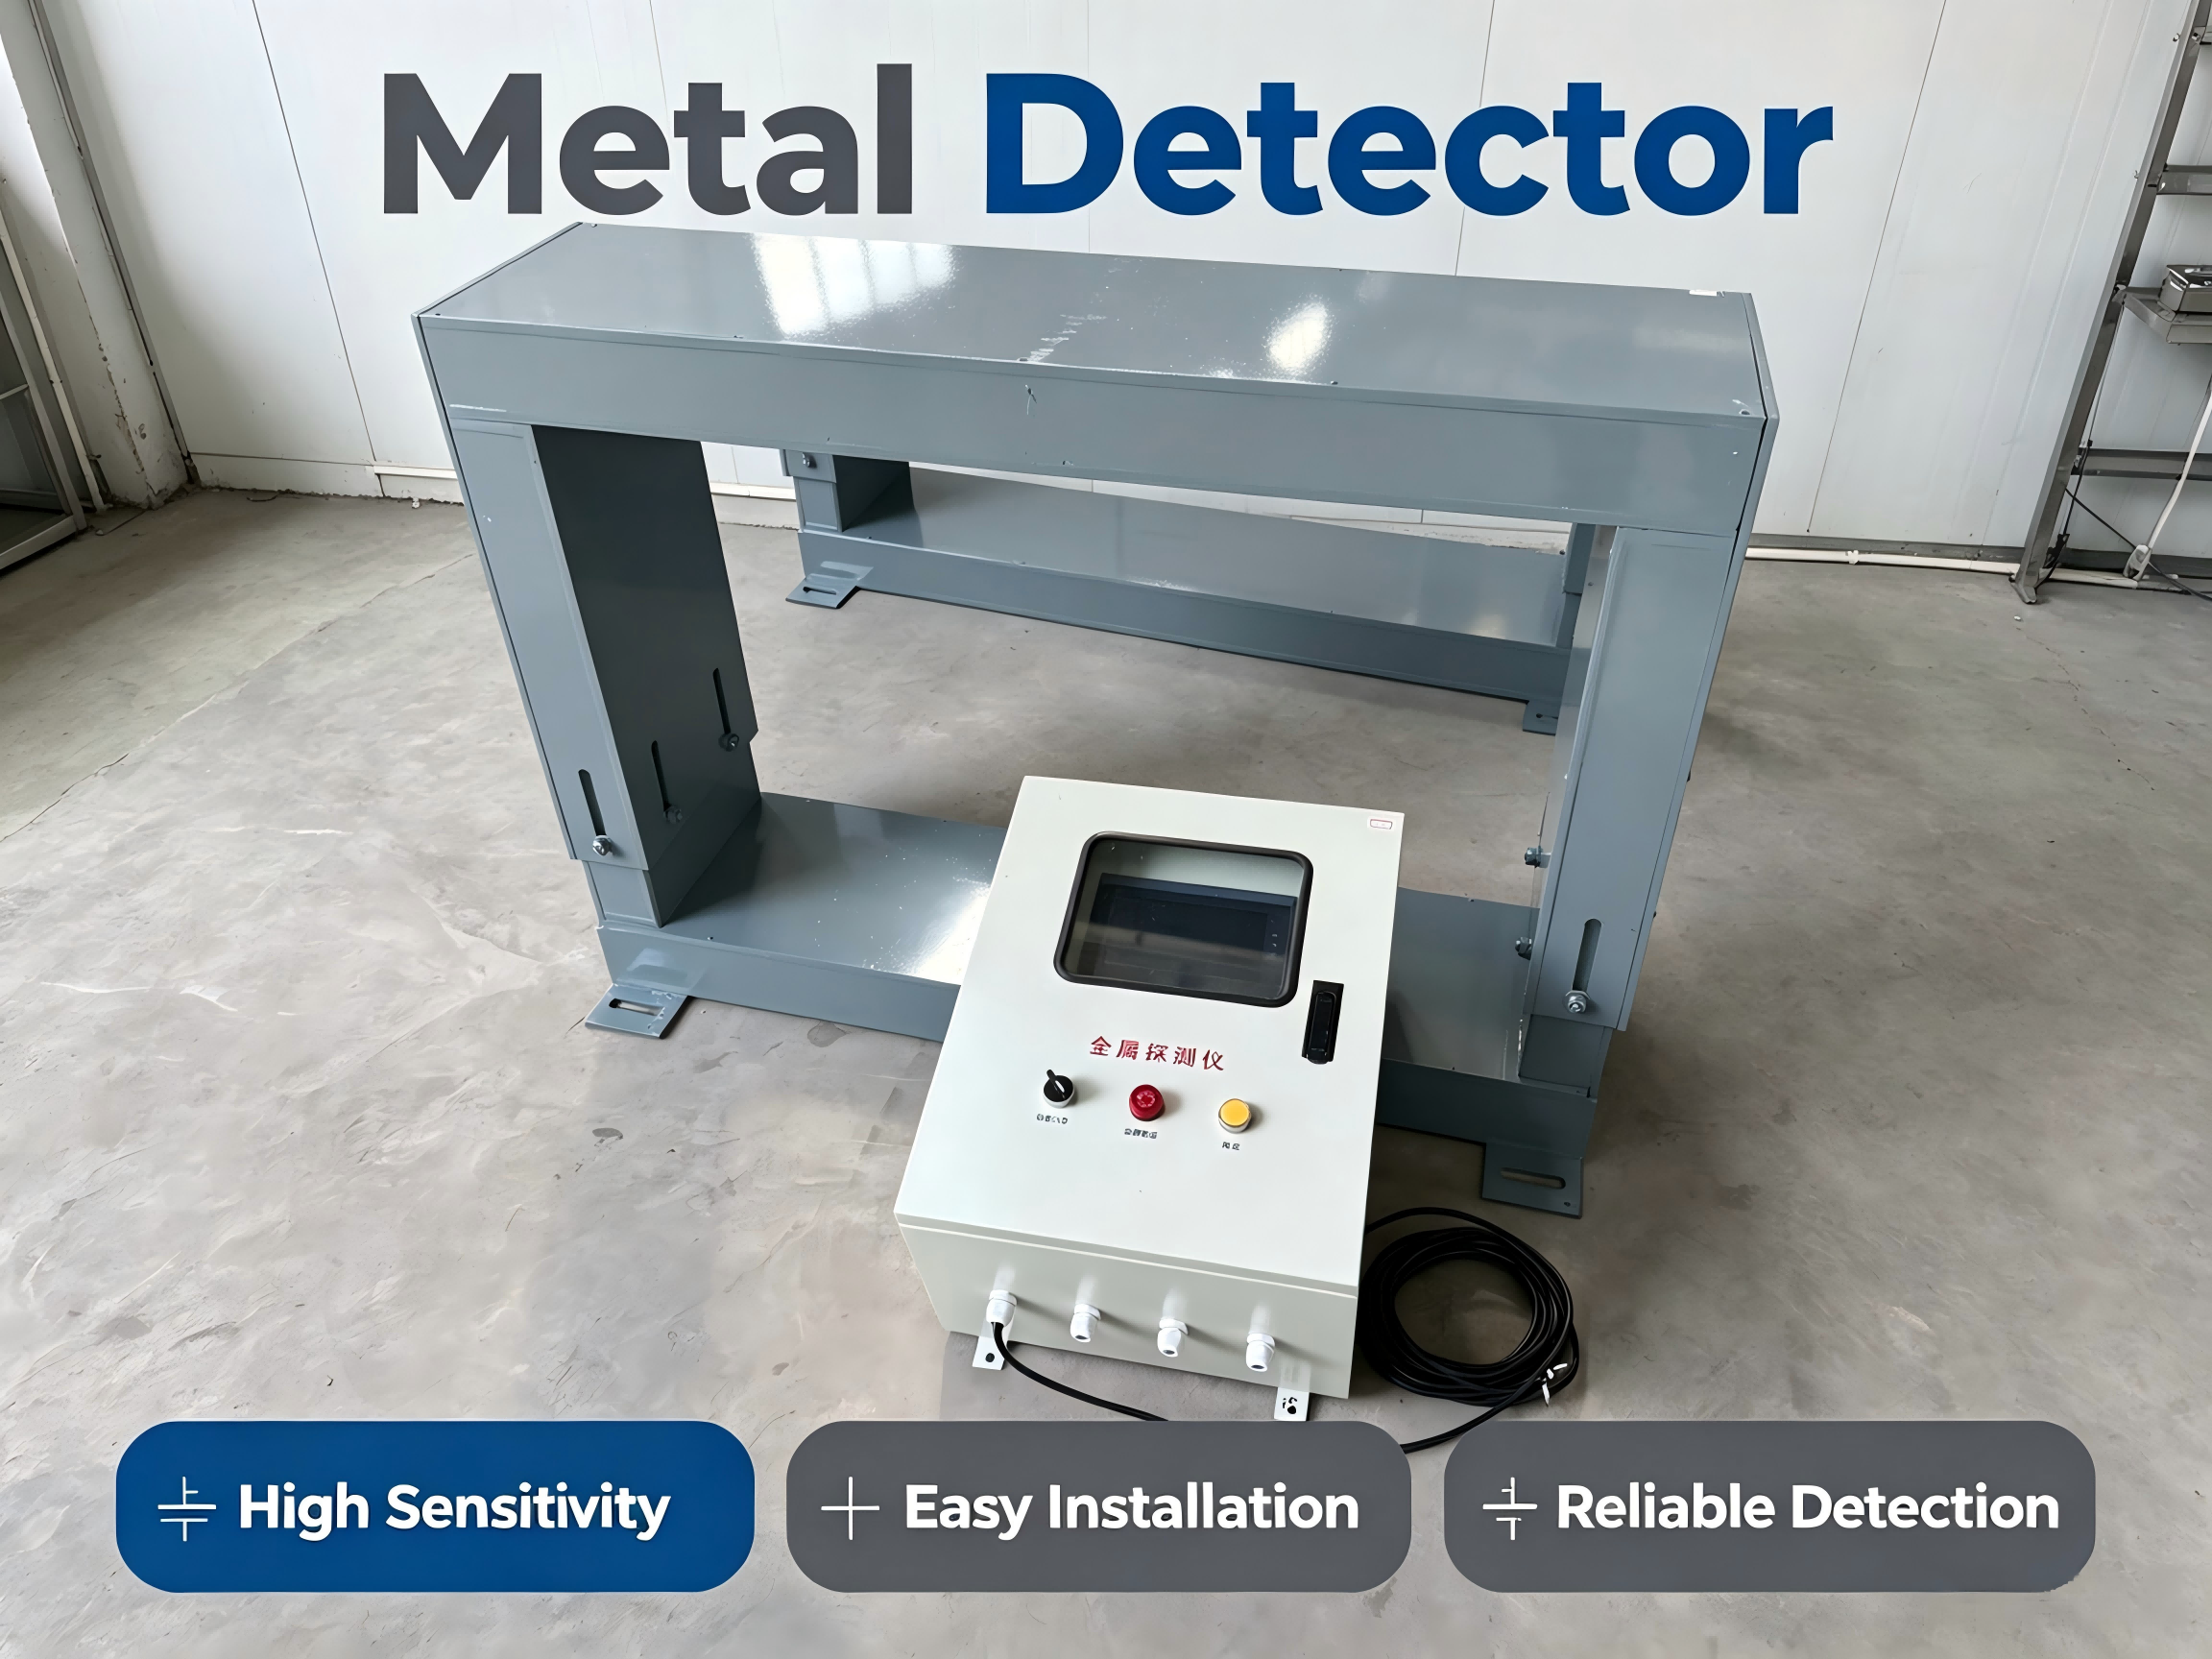
Metal Detector for Conveyor Belt Systems
Reliable Metal Detection for Continuous Material Handling
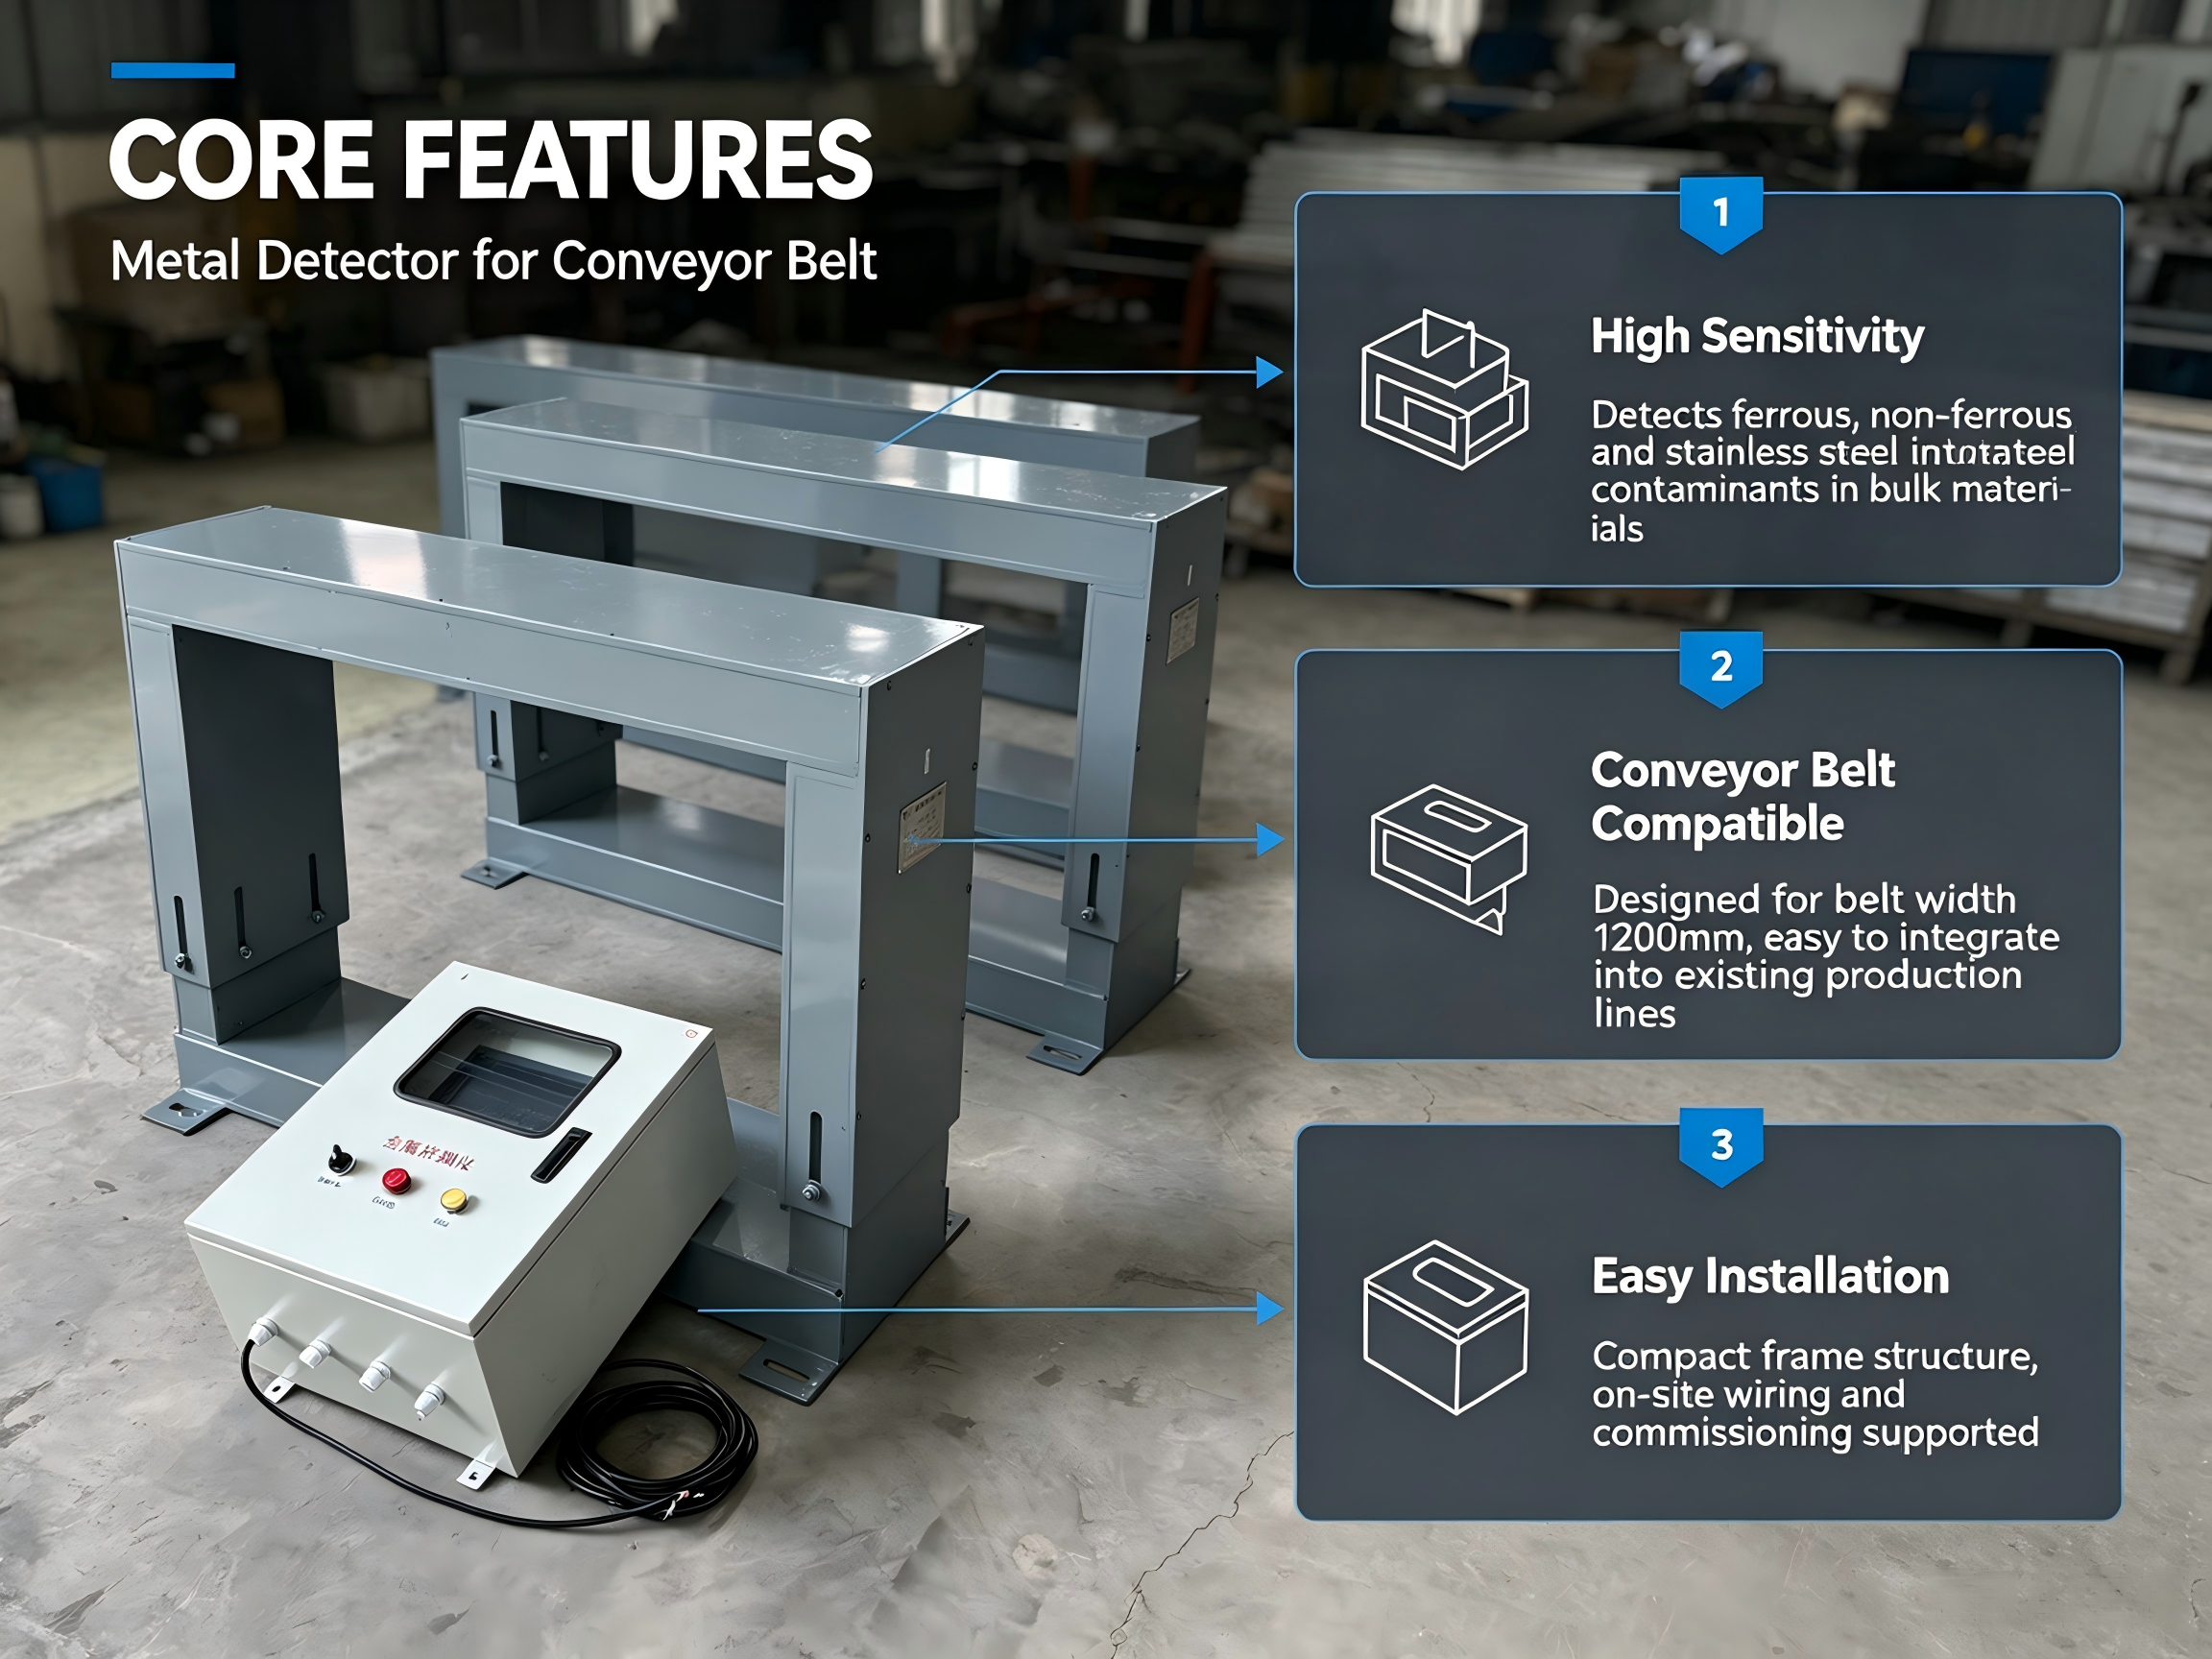
A Metal Detector is an important protection device used in conveyor belt material handling systems. It is designed to detect unwanted metal objects mixed into bulk materials and send an alarm or control signal when metal is detected.
Our conveyor belt metal detector is widely used in cement, mining, coal, metallurgy, chemical, power generation, aggregate, building materials and other industries. It can effectively detect ferrous, non-ferrous and weak magnetic metal contaminants while materials are continuously transported on a conveyor belt.
By installing a Metal Detector before crushers, mills, screens or other critical equipment, companies can reduce the risk of equipment damage, production interruptions and unexpected maintenance costs.
What Problems Can a Metal Detector Solve?
Metal contamination is a common problem in bulk material transportation. Bolts, nuts, steel pieces, tools, broken machine parts and other metal objects may accidentally enter the material flow.
When these objects reach a crusher, mill or other processing equipment, they can cause serious mechanical damage. In severe cases, the entire production line may need to stop for inspection and repair.
Our Metal Detector provides continuous online monitoring of the material flow. When unwanted metal is detected, the system can provide an audible or visual alarm and can also be integrated with the conveyor control system to stop the belt or activate a metal removal process.
This provides an additional layer of protection for expensive production equipment and helps improve the safety and reliability of the entire conveying system.
Applications
The conveyor belt metal detection system is suitable for a wide range of bulk material handling applications, including:
Cement plants
Mining and mineral processing
Coal handling systems
Metallurgy
Power plants
Chemical plants
Aggregate processing
Building materials
Sand and gravel plants
Crushing and screening systems
Bulk material transportation
It can be installed on belt conveyors, belt feeders and other continuous conveying equipment where real-time metal detection is required.
High Sensitivity Metal Detection
The system is designed to detect different types of metal materials, including magnetic metals, non-magnetic metals and weak magnetic metals.
Advanced electronic technology helps improve detection sensitivity and operational stability. The detection parameters can be adjusted according to the material characteristics, conveyor belt conditions and application requirements.
For industrial applications, stable detection performance is especially important because material properties, belt speed and environmental conditions can change during continuous production.
The Metal Detector is therefore designed for reliable operation in demanding industrial environments.
Main Features
1. Detects Different Types of Metals
The equipment can detect ferrous, non-ferrous and weak magnetic metal objects. This makes it suitable for different bulk material handling processes.
2. Continuous Online Detection
The detector monitors the material flow continuously while the conveyor is running. There is no need to manually inspect every batch of material.
3. Adjustable Detection Sensitivity
Detection sensitivity can be configured according to the application. This helps balance detection performance and stable operation.
4. Automatic Alarm
When metal is detected, the system can immediately generate an alarm signal. Depending on the production process, the signal can also be connected to the conveyor control system.
5. Equipment Protection
Installing a Metal Detector upstream of crushers, mills and other important equipment can help prevent damage caused by foreign metal objects.
6. Stable Industrial Operation
The system is designed for continuous operation and can be used in dusty, vibrating and demanding industrial environments.
7. Easy Operation and Maintenance
The control system is designed for convenient parameter adjustment, commissioning and daily operation, helping reduce maintenance difficulty.
Why Choose Our Metal Detector?
Compared with basic metal detection equipment, our conveyor belt detection solution focuses on the complete working environment of industrial bulk material handling.
The system can be configured according to conveyor width, belt speed, material characteristics, installation conditions and required detection sensitivity.
This project-oriented approach allows the Metal Detector to better match different production lines instead of using a one-size-fits-all configuration.
Another important advantage is system integration. The detector can work together with conveyor belts, belt feeders and plant automation systems, allowing metal detection to become part of the overall material handling and equipment protection system.