

Mining Metal Detector Working Principle
2026-10-29 15:34Mining Metal Detector
Product Introduction and Working Principle
1. Product Introduction
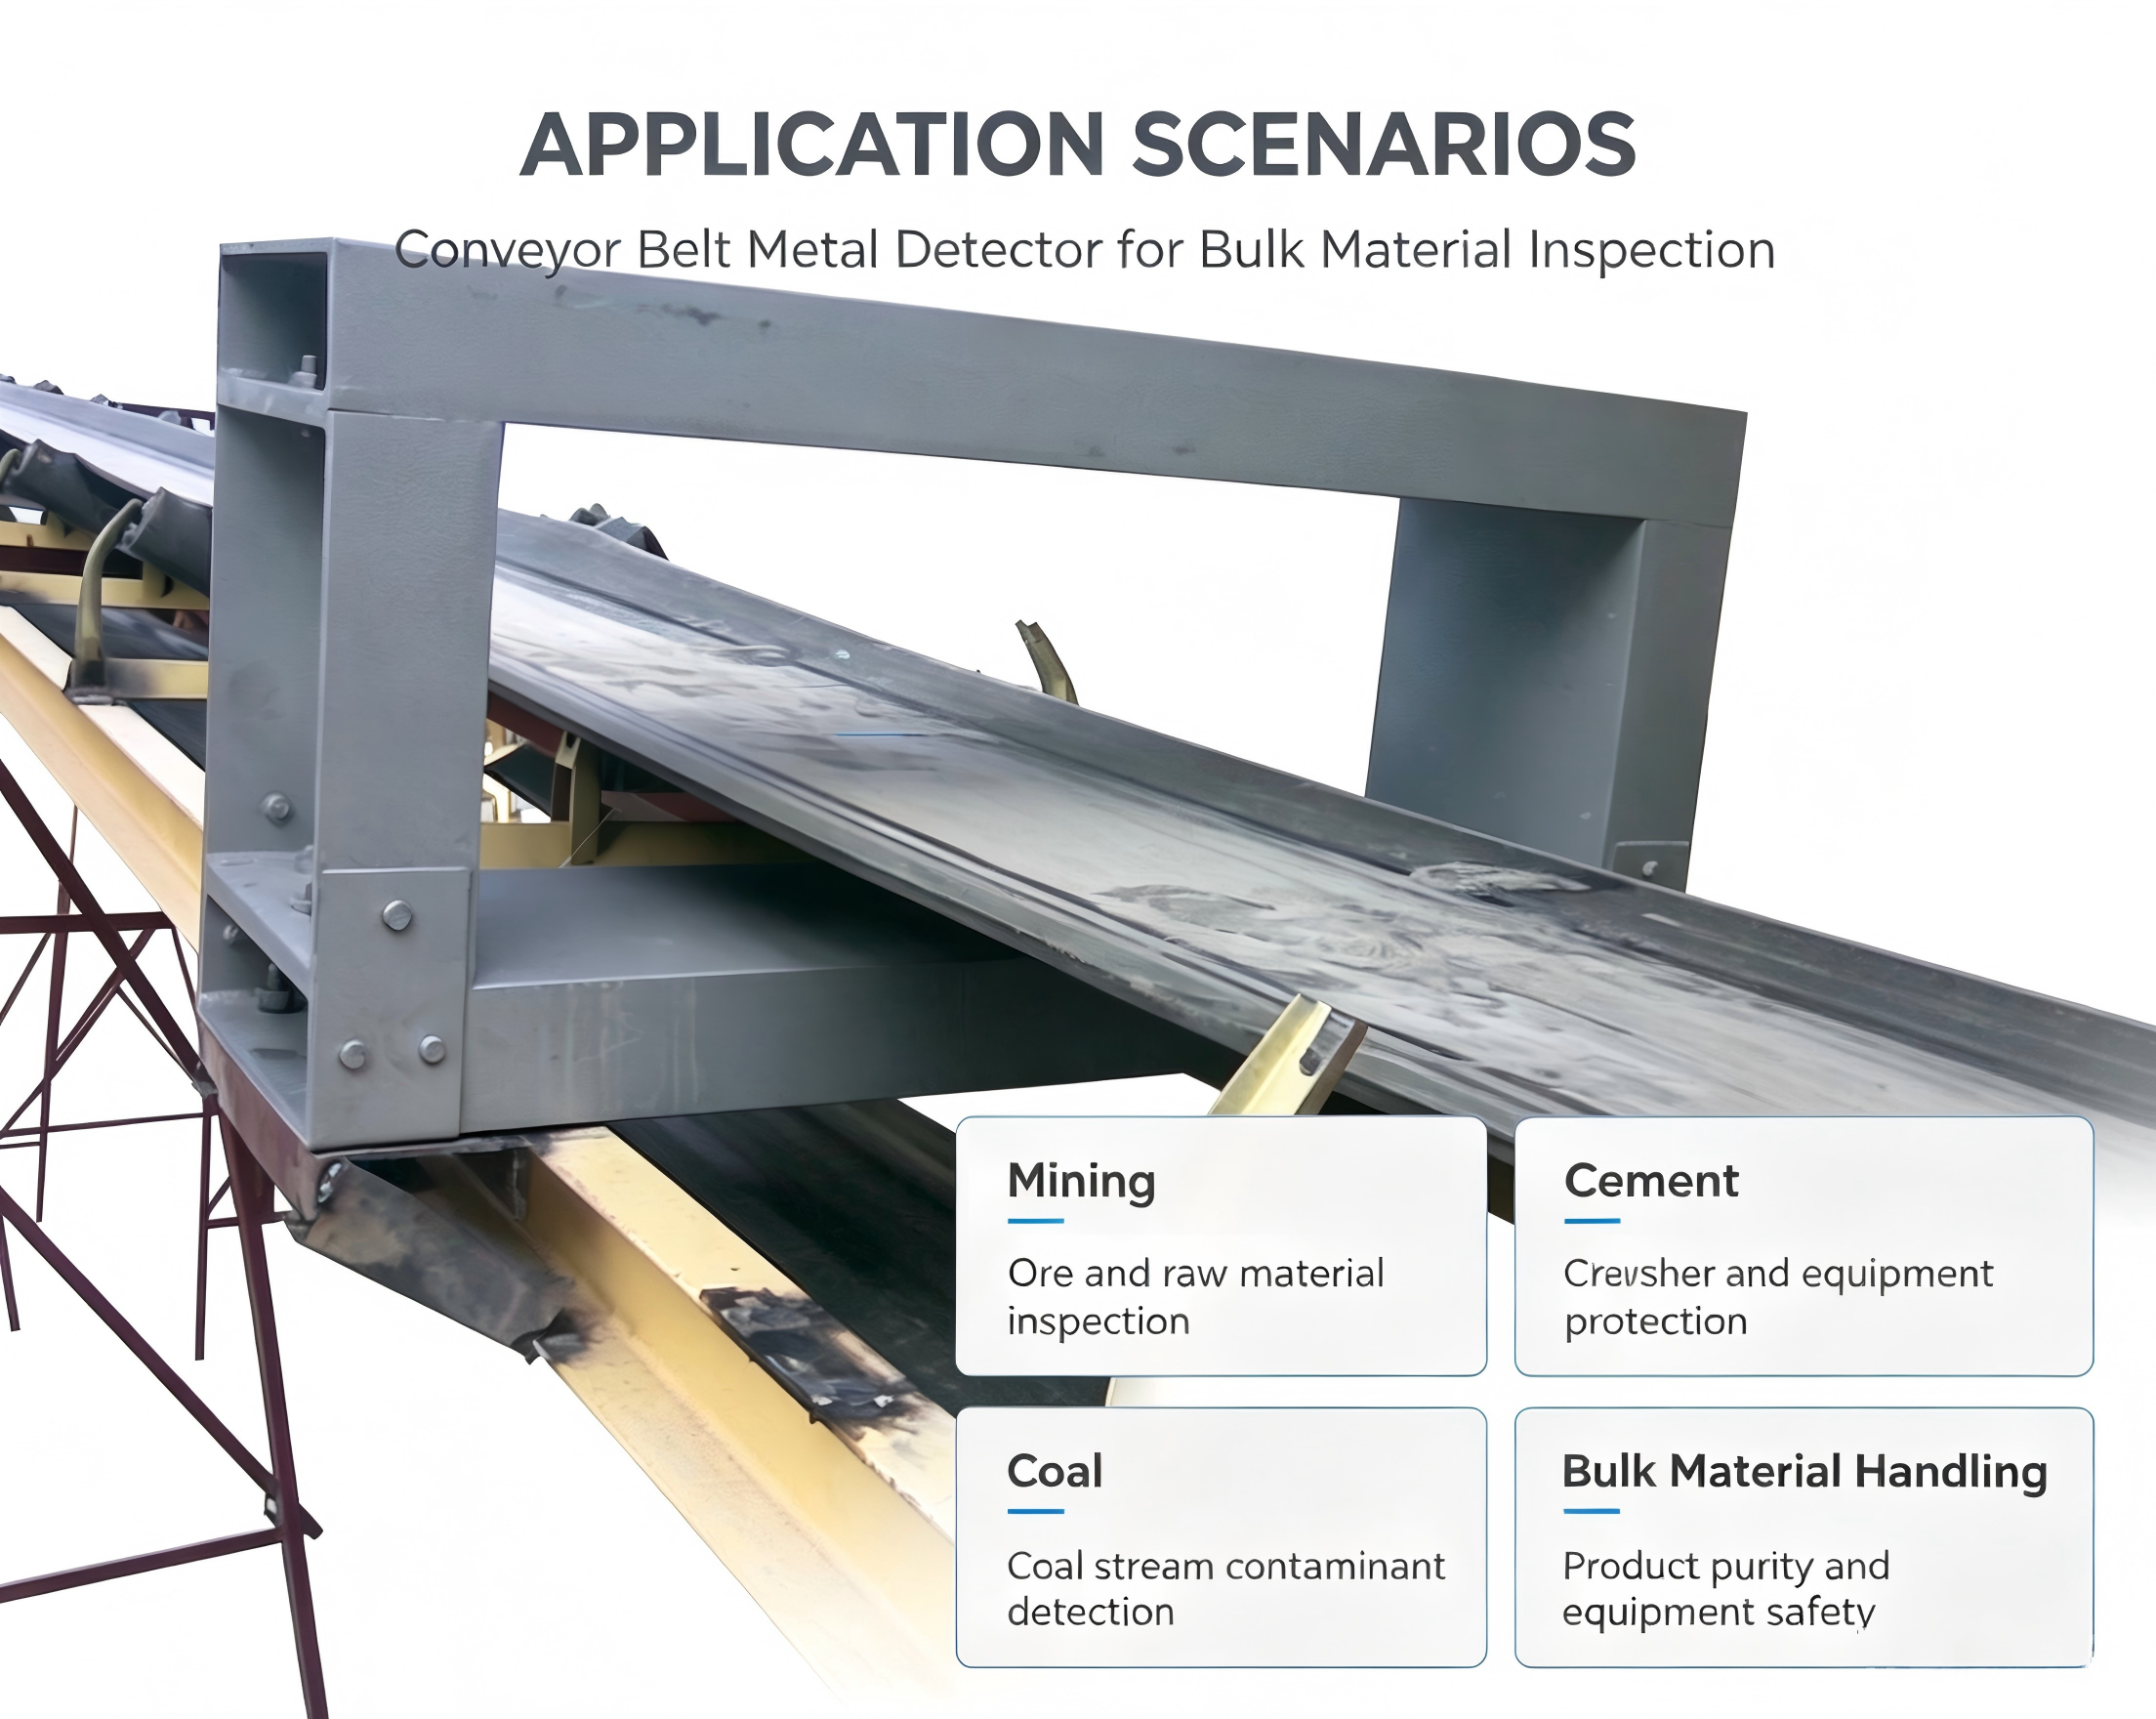
The Mining Metal Detector is an industrial detection device designed to identify unwanted metal contaminants in bulk materials transported by conveyor belts. The equipment is widely used in mining, cement, coal, metallurgy, power generation, and other material handling industries.
During mining and material processing, iron pieces, steel scraps, broken drill bits, and other metal objects may enter the conveyor system along with the raw materials. These contaminants can damage crushers, mills, conveyors, and other production equipment. Installing a Mining Metal Detector helps detect metal contamination before it reaches critical machinery, reducing equipment damage, unexpected downtime, and maintenance costs.
The system can detect both magnetic and non-magnetic metal objects, depending on the detector design and operating conditions. With adjustable sensitivity, stable detection performance, and integration with conveyor control systems, the Mining Metal Detector provides reliable protection for continuous industrial production lines.
2. Working Principle of Mining Metal Detector
The Mining Metal Detector generally operates based on electromagnetic induction. Its working process involves the following steps:
Electromagnetic field generation: The detector coil generates an electromagnetic field within the detection area of the conveyor belt.
Metal object detection: When a metal object passes through the detection zone, it disturbs the electromagnetic field and produces a detectable signal.
Signal processing: The control unit analyzes the signal and determines whether the detected object meets the preset sensitivity threshold.
Alarm or control output: When metal is detected, the system can activate an audible or visual alarm, stop the conveyor, or send a signal to an automatic metal removal device.
Production line protection: The control system helps prevent metal contaminants from entering downstream crushers, mills, and other processing equipment.
Detection sensitivity depends on the metal type, object size and shape, conveyor speed, material characteristics, installation conditions, and detector settings.
3. Main Features
High detection sensitivity: Detects unwanted metal contaminants in bulk materials under suitable operating conditions.
Reliable operation: Designed for continuous industrial conveying and material processing applications.
Adjustable sensitivity: Allows detection parameters to be configured for different materials and production requirements.
Automatic alarm function: Provides alarm signals when metal contamination is detected.
System integration: Can connect with conveyor belt control systems, alarms, and compatible metal separation equipment.
Easy operation and maintenance: A control cabinet supports parameter adjustment, status monitoring, and routine inspection.
4. Applications
Mining Industry
Detects metal contaminants in iron ore, copper ore, and other mineral materials to protect crushers, grinding mills, and conveying equipment.
Coal and Power Plants
Identifies metal objects mixed with coal before the material enters crushers and other coal processing equipment.
Cement Industry
Helps prevent scrap iron and steel fragments from entering raw material grinding systems and other critical production equipment.
Aggregate and Metallurgical Industries
Provides metal contamination monitoring for stone crushing, mineral processing, and bulk material transportation.
5. Why Choose Weifang Zhitian Mining Metal Detector?
Weifang Zhitian provides industrial metal detection and material handling equipment for mining and bulk material processing applications. The Mining Metal Detector can be selected according to conveyor width, material characteristics, belt speed, detection requirements, and production line configuration.
The detector can be integrated with compatible alarm, conveyor shutdown, and metal removal systems to help improve production safety and equipment reliability. Customized solutions are available to meet different industrial operating conditions.
Conclusion: The Mining Metal Detector is an important protective device for conveyor-based production lines. By detecting unwanted metal contaminants early and triggering appropriate control actions, the system helps reduce equipment damage, improve operational reliability, and maintain continuous material handling.